A turned part often doesn't leave the machine as a blank. It leaves as a finished part. DFP Pott GmbH turns, mills, and drills in a single setup, with driven tools and a sub-spindle, programmed AI-assisted directly at the machine. Fewer reclamps, fewer reference errors, shorter lead times.
Driven tools on the main and sub-spindle turn turning into more than turning. DFP Pott GmbH runs turn-mill complete machining: turning, milling, and drilling operations in a single setup. The part is finished on the sub-spindle, without reclamping. What leaves the machine is finished, not half-finished.
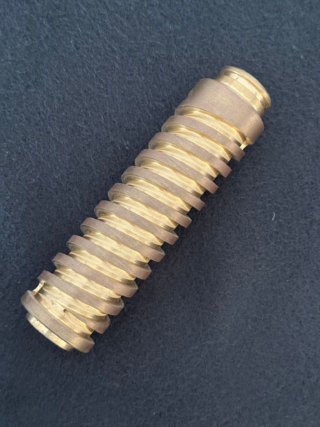
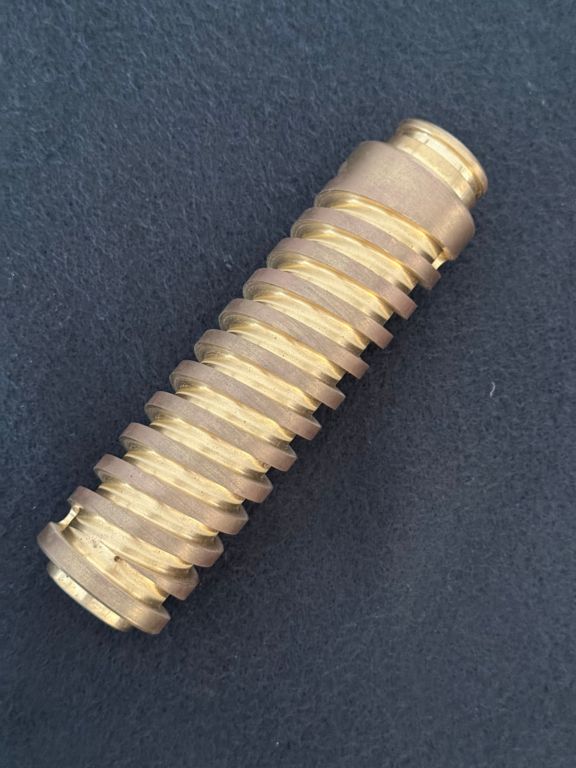
From the short pin to the long shaft. DFP Pott GmbH turns precision parts from metal, non-ferrous metal, and engineering plastic, with a bar feeder for economical batch production and single-setup work for the special part. Where tight bearing and sealing fits are required, the part moves on to grinding without changing shops.
In hard turning, DFP Pott GmbH machines parts that are already hardened, using a geometrically defined cutting edge. The process typically starts at 45 HRC and, depending on material, geometry, and task, also suits considerably higher hardness. Typical materials are bearing steels such as 100Cr6, case-hardened gear steels, and hardened alloy steels such as 42CrMo4. Cutting materials and tool geometries are matched to hard machining.
Hard turning does not replace cylindrical grinding as a rule. It saves operations: contours, grooves, faces, and cylindrical surfaces are machined in one setup, and reclamping is eliminated. If the drawing calls for maximum roundness, form accuracy, or surface finish, grinding follows. At DFP Pott GmbH, turning and grinding run in the same shop. The process sequence follows your workpiece: short paths, coordinated processes, one contact.
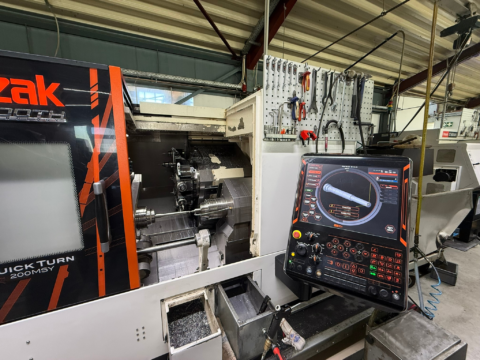
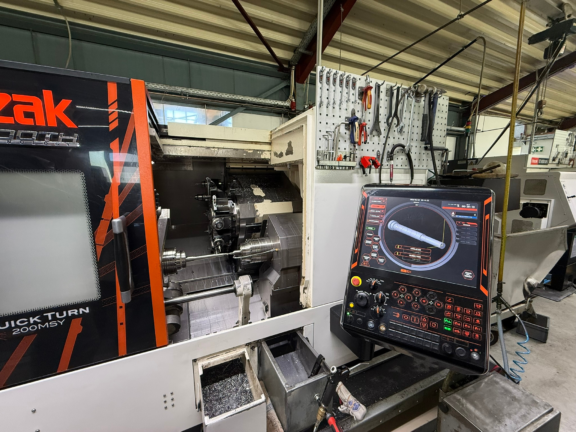
Whether single part, small batch, or ongoing series: DFP Pott GmbH turns to drawing, STEP file, or a sample part. S355 and 42CrMo4 are held in stock, express delivery available. Stainless steels, titanium, and special alloys are sourced actively.
Every turned part is documented and fully measured on request. On request, you receive a First Article Inspection Report (FAIR) and dimensional report, audit-ready to DIN EN ISO 9001:2015.
A STEP file and drawing, or a sample part: that is enough to start. DFP Pott GmbH checks feasibility and lead time and responds with a binding estimate.
Yes. DFP Pott GmbH turns, mills, and drills in a single setup, with driven tools and a sub-spindle. The part is finished without reclamping, which reduces reference errors and shortens lead time. Where needed, the part moves on to grinding without changing shops.
DFP Pott GmbH turns metals, non-ferrous metals, and engineering plastics. S355 and 42CrMo4 in Ø 10–65 mm are held in stock, express delivery available. Stainless steels, titanium, and special alloys are sourced actively and available at short notice.
Yes. DFP Pott GmbH turns single parts, small batches, and ongoing series to drawing, STEP file, or a sample part. A bar feeder enables economical batch production; single-setup work covers the special part. Every part is documented to DIN EN ISO 9001:2015.
Yes. DFP Pott GmbH turns hardened parts with a geometrically defined cutting edge, typically from 45 HRC. Typical materials are 100Cr6, case-hardened gear steels, and hardened 42CrMo4. If the drawing calls for maximum roundness or surface finish, cylindrical grinding follows in the same shop, without changing companies.